We combine modern rice milling technology, optical sortex color sorting, climate-monitored warehousing, and seamless ocean logistics to deliver world-class rice to 50+ countries.
.1792659103.jpg)
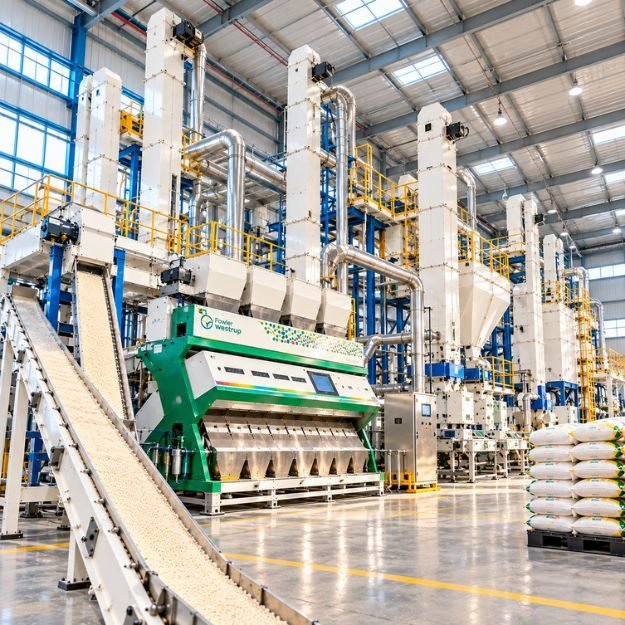
Our ultra-modern processing mills are engineered for high yield and zero grain breakage. We process a wide variety of Basmati and Non-Basmati rice, maintaining natural aroma, grain length, and uniform texture.
Purity is non-negotiable. Our high-speed optical color sorters use high-resolution CCD cameras and infrared sensors to detect and eliminate foreign particles, chalky grains, and color defects at microscopic speeds.
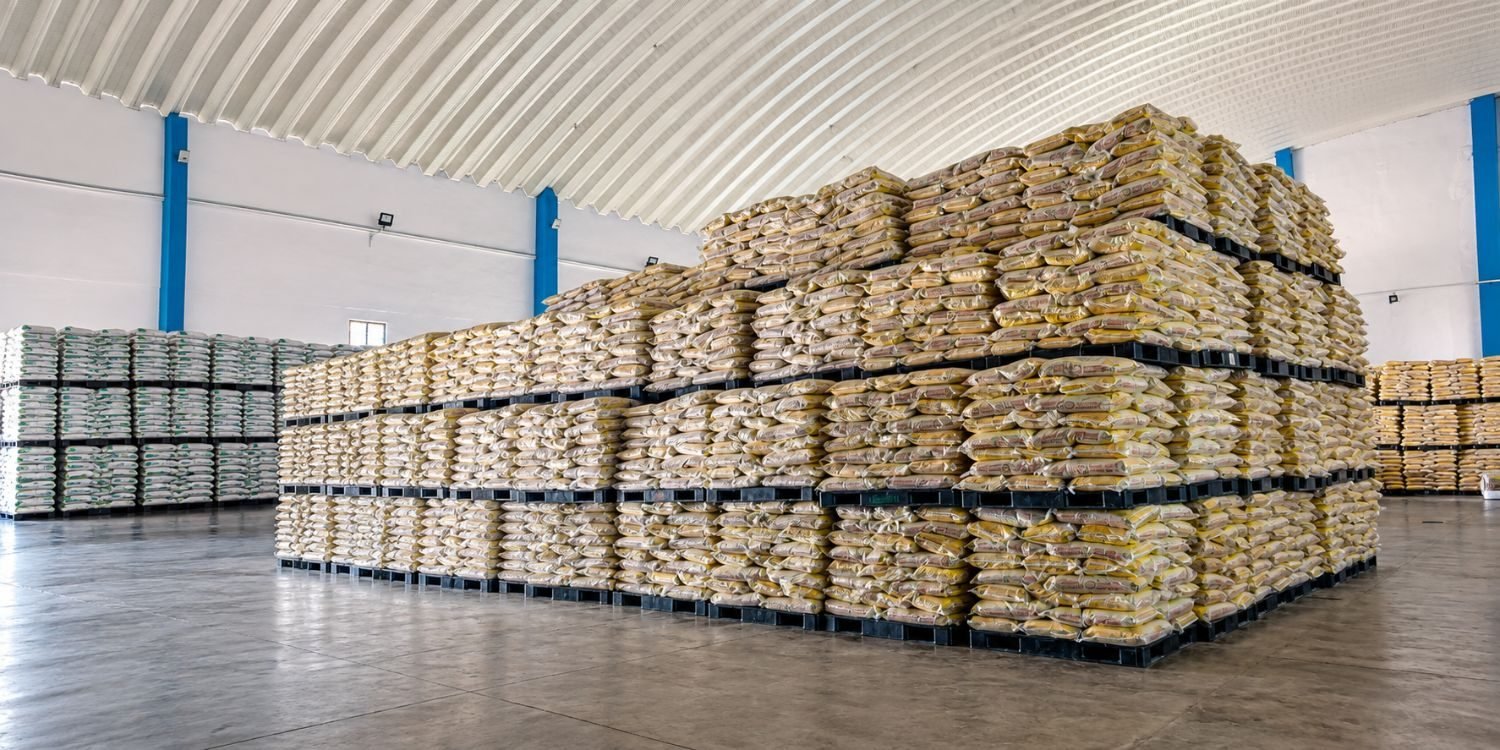
Our climate-controlled warehouses preserve grain freshness and prevent infestation. Located near Kandla & Mundra sea ports, our storage facilities ensure quick container loading and smooth shipping logistics.
We export rice to over 50 countries across North America, Europe, Middle East, Africa, and Asia. We offer customized consumer and bulk packaging with full private label printing.
.1792659103.jpg)
Every shipment undergoes stringent laboratory testing and inspection before leaving our facility.
Direct procurement of high-grade paddy from trusted farming regions, tested for grain moisture and purity.
Multistage de-husking and polishing machines extract flawless rice grains while preserving aroma.
Camera sensors sort discolored kernels to guarantee 99.9% color purity and uniform grain length.
Automatic packaging in customized bags, palletized and loaded into ocean containers for shipping.